The short answer
Most flexible LED strips are made by printing solder paste onto a flexible printed circuit board (FPCB), placing LEDs and other surface-mount components, soldering them in a controlled reflow oven, inspecting and electrically testing the assembled board, joining or cutting it to length, applying any required protective construction, and completing final testing and packing.
That sequence sounds simple. The difficult part is controlling the inputs and the process: copper and PCB construction, LED and resistor identity, solder-paste deposit, placement accuracy, reflow profile, color bin, operating current, waterproofing, joints, labels and inspection criteria. A buyer should approve those details before mass production, not discover them from a finished reel.
The exact route varies by product. COB tape, conventional SMD tape, long-run high-voltage tape and silicone-extruded outdoor strip do not share every operation. The steps below describe a typical workflow and the purchasing controls attached to it.
1. Freeze the specification and incoming materials
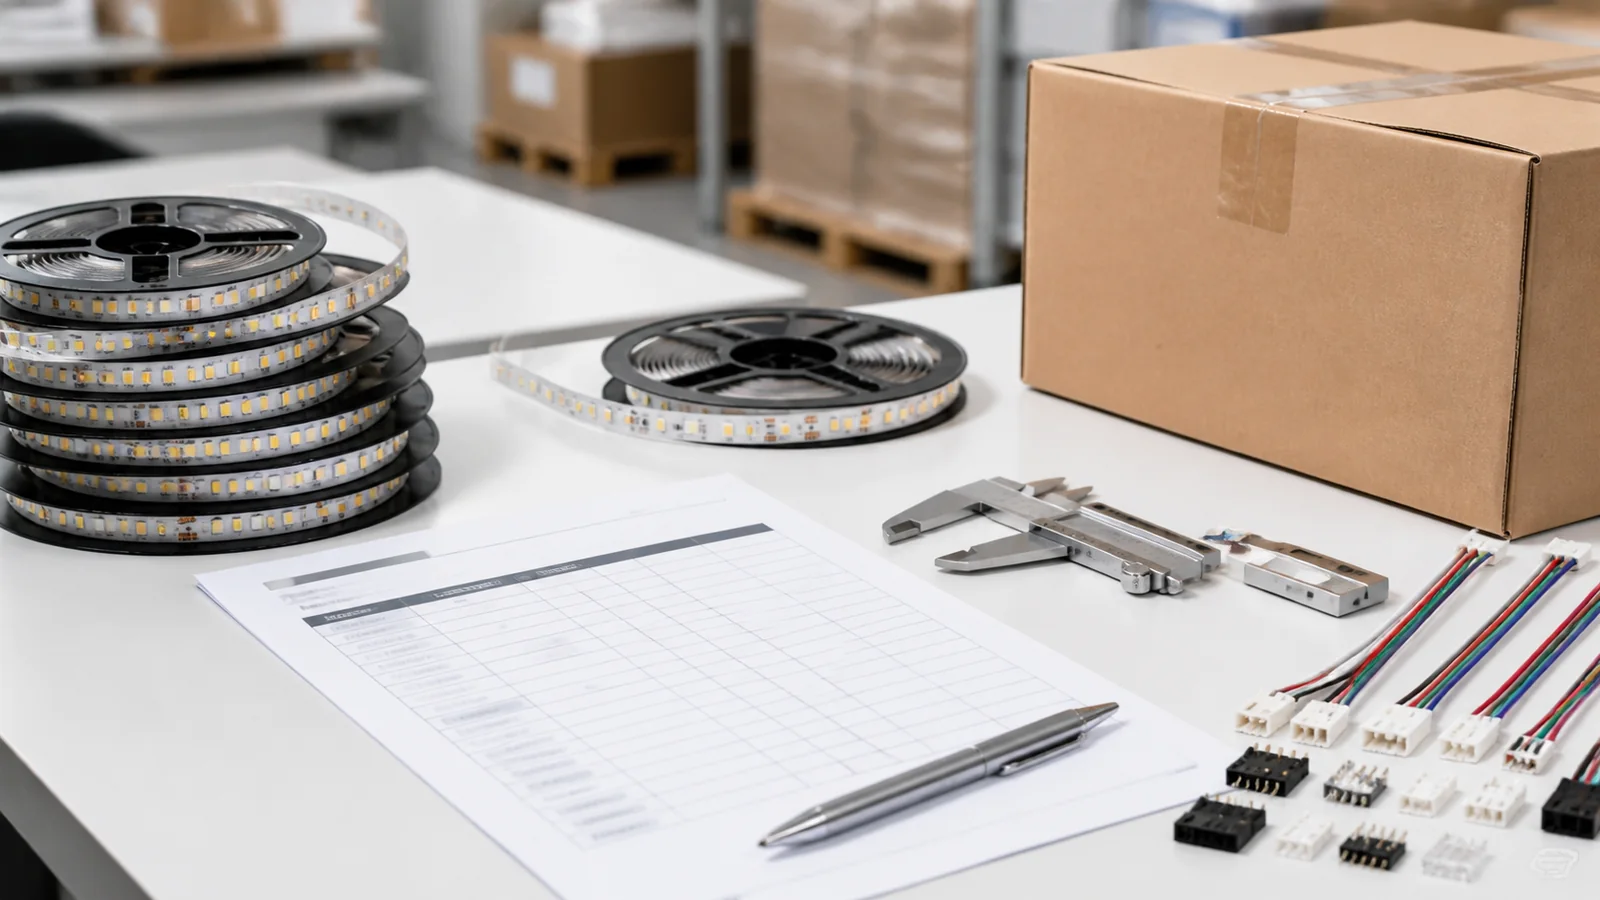
Production should begin from a controlled model specification or approved sample. At minimum, it should identify:
- circuit voltage and electrical architecture;
- LED package or COB construction, density and color channel arrangement;
- PCB width, copper and layer construction where required;
- watts per meter and permitted tolerance;
- CCT or color coordinates, CRI and color-tolerance requirement;
- cut interval, reel length and connection method;
- IP construction, coating or extrusion detail;
- label, packaging and destination-market documentation.
A line name such as “2835 120 LED” is not enough. Different chips, PCB constructions and drive currents can produce different output, heat and service life under the same marketing name.
Incoming inspection may verify material identity, dimensions, lot information, moisture-sensitive handling requirements and supplier documents. The checks should match the model risk. For example, a color-critical retail order needs a defined LED bin control, while an outdoor order needs particular attention to silicone, cable, connector and sealing materials.
If the project uses private labels, complete the technical model before approving printed claims. The OEM service workflow separates product decisions from label and carton decisions so packaging does not lock in an unverified specification.
2. Print solder paste, place components and reflow
Solder-paste printing
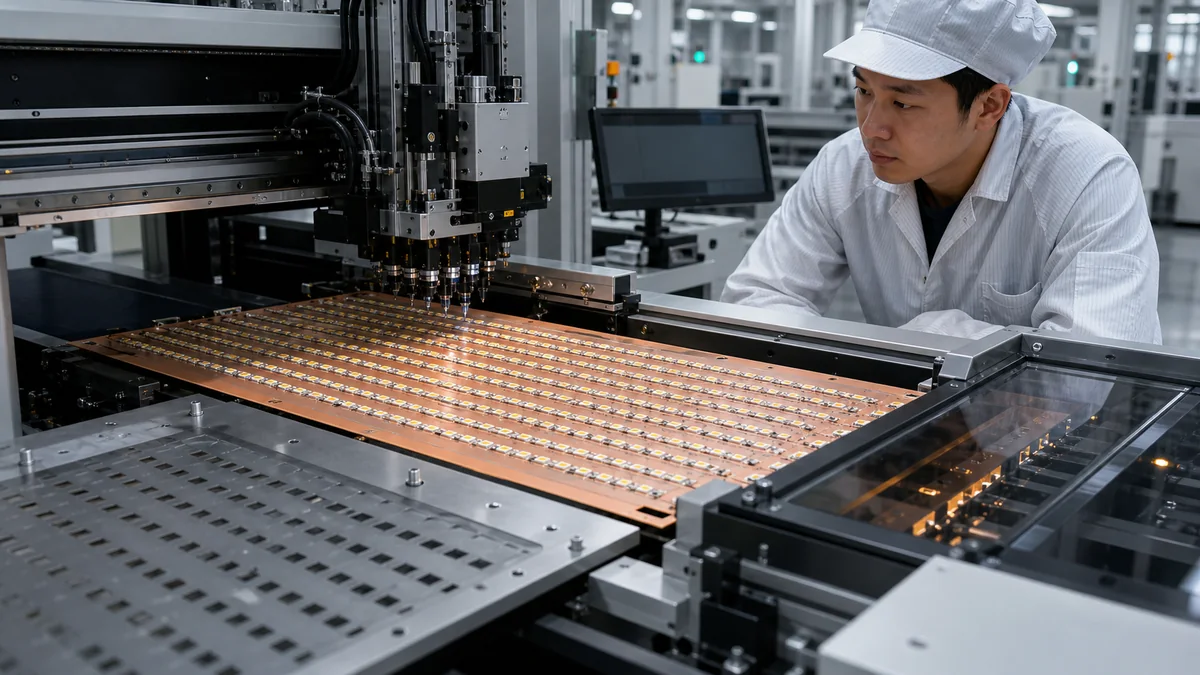
The FPCB panel is aligned under a stencil and solder paste is deposited on the component pads. Deposit volume and alignment matter: too little paste can create weak or open joints; too much can contribute to bridging or displaced components. Paste condition, stencil cleanliness and print inspection are process controls rather than cosmetic details.
Pick-and-place
Automated placement equipment picks LEDs, resistors and control components from reels and places them on the pasted pads. The machine program must match the board and component orientation. Feeder setup, nozzle condition and placement depth matter, especially with small or mechanically sensitive LED packages.
Nichia’s official LED mounting process application note explains how stencil printing, placement pressure and reflow conditions interact. It is component guidance, not a universal recipe: the selected LED manufacturer’s data sheet and assembly instructions remain the controlling reference.
Reflow soldering
The populated FPCB passes through a reflow oven. The solder paste melts and forms the electrical and mechanical joints, then cools. A suitable temperature profile depends on the solder paste, LED package, board construction, loading and equipment. It should be established and monitored for the actual assembly.
This is not a step where “hotter is safer.” Cree LED’s soldering and handling guidance warns that excessive heating rate can damage LEDs and instructs users to follow product-specific conditions. A factory process should therefore retain a qualified profile rather than copy one peak-temperature number from an unrelated component.
Post-reflow inspection
Automated optical inspection or visual inspection can identify missing, rotated or displaced components, solder bridges and visible joint defects. Inspection does not prove every hidden electrical or material property, so it is paired with electrical and optical tests.
3. Test, join, protect and finish the strip
Electrical and lighting checks
The assembled panel is powered under a defined condition to find opens, shorts, wrong-color channels and abnormal sections. Depending on the order, checks may include current or power per meter, light output, CCT, color coordinates, CRI and visual uniformity. The instrument, test length, stabilization time, input voltage and tolerance must be stated if the result is an acceptance criterion.
For multi-batch or adjoining installations, specify the permitted color difference before ordering. The SDCM and binning guide explains why a CCT label such as “3000K” does not by itself control visible batch variation.
Joining, cutting and reel preparation
Panels or long strip sections may be separated, joined, soldered or fitted with connectors according to the finished length. Operators should control pad damage, polarity, joint shape, insulation and strain relief. A powered visual check after joining helps catch a fault introduced after the first board test.
Protective construction
Indoor IP20 tape may proceed directly toward adhesive application and packing. Protected models can add conformal coating, tube, glue filling or silicone extrusion. Ends, cable exits and field joints need their own sealing method.
An IP rating applies to the tested enclosure or construction, not automatically to every cut end and accessory. Use the IP20, IP65 and IP68 guide to specify the complete installed system.
Aging or burn-in
An aging test can reveal early failures and unstable joints, but “aged” is not a complete test specification. Buyers should define or confirm the model, test length, input condition, duration, mounting state and acceptance criteria. Do not assume that a photograph of illuminated reels proves the same test was applied to the ordered batch.
Final inspection and packaging
Final inspection confirms the released model against the order: appearance, operation, length, labels, accessories, quantity and packing. Sampling level and acceptance criteria should be agreed before inspection. The pre-shipment AQL checklist shows how to separate critical, major and minor defects instead of relying on “general inspection passed.”
Packaging must protect the reel, components and waterproof construction through the actual shipping route. For wholesale orders, define reel restraints, moisture controls where required, inner box, carton, barcode ownership and pallet rules in a packaging specification.
The buyer's control point at each stage
| Production stage | Common risk | Evidence or check to request |
|---|---|---|
| Specification release | Buyer and factory quote different constructions under one name | Signed data sheet, drawing and approved sample reference |
| Incoming materials | Uncontrolled LED bin, PCB or protective material substitution | Material/lot traceability required by the purchase specification |
| Paste and placement | Insufficient paste, bridge, polarity or placement error | Print/placement controls and post-reflow inspection record |
| Reflow | Poor joint or package stress from unsuitable profile | Qualified model-specific profile and line control record where required |
| Electrical/optical test | Test performed at a different voltage, length or temperature | Test method, equipment, conditions and tolerance |
| Joining and connectors | Pad damage, reversed polarity, weak joint, no strain relief | Workmanship standard and powered inspection after joining |
| Waterproof finishing | End seal or cable entry weaker than the strip body | Approved construction sample and model-specific ingress evidence |
| Aging | Undefined or decorative “lighting test” | Agreed condition, duration, batch identification and acceptance rule |
| Final QC | Sampling cannot detect agreed critical defects | Inspection plan, AQL or 100% check where risk justifies it |
| Packing | Reel deformation, abrasion, moisture or label mismatch | Approved packaging sample and carton specification |
Product labels and cartons should be released only after the model, electrical ratings, reel length, batch code and ordered configuration are frozen. Artwork must match the signed specification and approved sample.
Questions to ask an LED strip factory
- Which data sheet revision and approved sample control this order?
- Which parts of the BOM are fixed, and which substitutions require buyer approval?
- How are LED bins and production lots identified for repeat orders?
- What are the electrical and optical test conditions and tolerances?
- How is the reflow profile qualified for the selected LED and FPCB assembly?
- Which defects are checked automatically, visually and electrically?
- How are strip joints, polarity, end seals and cable entries inspected?
- What aging condition is used for this exact model, if aging is specified?
- Which checks are 100%, and which use sampling?
- How will inspection results, carton labels and batch traceability be delivered?
Our factory overview shows the production and QC areas supporting current supply. For an order-level review, send the model, destination market, quantity, application, drawing and inspection requirements through the quotation form. The useful outcome is a controlled specification and inspection plan—not a generic promise that every strip follows the same process.
Catalog & Sourcing Note
This article is prepared from our current product catalog and B2B specification workflow. Electrical, waterproofing and installation requirements vary by model and market, so confirm the final specification and approved sample before ordering.
Discuss Your Specification