The short answer
Approve an LED strip sample only after it is tied to a written model specification, test condition and revision. Check the strip, driver or rectifier, controller, connectors, mounting method and packaging that the bulk order will actually use. Keep one sealed reference sample and a signed approval record; then require the production lot and pre-shipment inspection to match them.
A sample can confirm fit, appearance and system behavior under defined conditions. It cannot by itself prove batch consistency, long-term life, waterproof performance or the quality of thousands of meters. Those questions need production controls, written acceptance limits and appropriate testing.
First decide which sample you are approving
Suppliers and buyers often use the word “sample” for different things. Label the stage clearly.
| Sample stage | Purpose | What it does not prove |
|---|---|---|
| Stock evaluation sample | Screens a product family and supplier response | Final branding, batch or production construction |
| Engineering sample | Confirms a proposed electrical or mechanical change | Stable mass-production process |
| Pre-production sample | Represents the frozen order specification before the run | Shipment-wide consistency |
| Packaging sample | Confirms reel, bag, label, box and carton execution | Electrical and optical performance unless included |
| Shipment sample | Supports final comparison or retention | A statistically representative inspection on its own |
If the first sample uses available PCB, temporary wire or plain packaging, record every difference. Do not allow a convenient stock sample to become the silent specification for an OEM order.
For custom work, the most important approval is normally the pre-production sample made after the model, materials, color target, cable, connector, label and packaging details are frozen.
Build one approval pack, not a trail of chat messages
The sample should have an identification label that links it to a controlled approval pack. Include:
- supplier and buyer model codes;
- specification revision and approval date;
- voltage, rated watts per meter, color type and control method;
- LED package or COB construction, LED density and PCB width;
- color target and agreed tolerance or bin control;
- IP construction, where applicable, including cable entry and end treatment;
- cut interval, reel length, adhesive or mounting method;
- wire length, connector type, polarity and pin order;
- driver, rectifier or controller used during approval;
- label, bag, inner-box and carton artwork revisions;
- photographs of the approved lit and unlit sample;
- deviations that are temporarily accepted or still open.
Use exact model-specific limits. “Waterproof,” “high CRI” or “premium PCB” is not an approval limit. The buyer must know which construction, values and tolerances apply to the ordered model. Record them in the signed specification and retained sample.
What to test on an LED strip sample
Identity and construction
Start with the unpowered strip. Compare the PCB marking, width, LED or COB arrangement, component layout, copper pads, cut marks, solder joints, wire entry, coating or extrusion and backing adhesive with the data sheet. Measure dimensions with suitable tools and record the method.
For protected products, confirm the complete construction rather than inspecting only the illuminated surface. End caps, injection points, cable exits and connectors can be the weak part of an outdoor assembly. A sample splash or immersion demonstration is not a substitute for a model-matched IP test report.
Electrical behavior
Test at the specified voltage with compatible equipment. Record input voltage at the strip, current or power under the agreed condition, startup behavior, operation after warm-up and performance at representative run lengths. For color-changing products, exercise every channel and the intended controller protocol.
Do not accept a power reading without its conditions. Reel length, feed arrangement, warm-up time, instrument accuracy and measurement point can change the result. A measured difference may be caused by the sample, the supply, the wiring or the procedure.
Light appearance and optical data
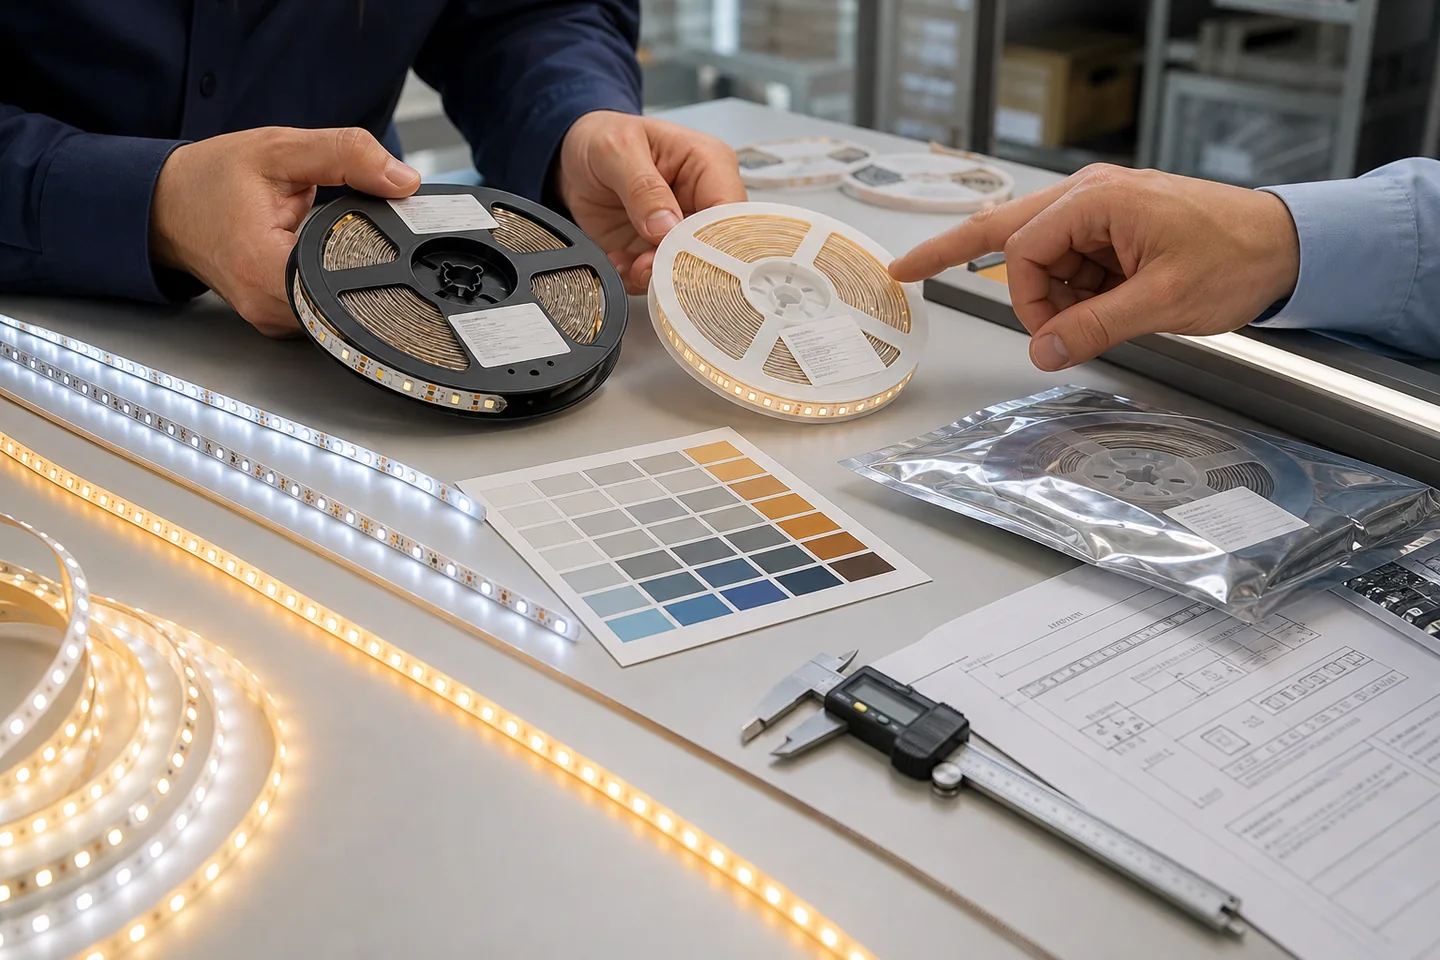
View samples side by side on the intended mounting surface, profile and diffuser. Use the actual viewing distance and ambient light where possible. Check:
- continuous light appearance and visible LED dots;
- color difference between sections and reels;
- brightness uniformity from feed end to far end;
- color mixing and channel balance for tunable or RGB products;
- diffuser interaction, glare and reflected surface appearance.
Visual comparison is useful, but it does not replace measured limits. For projects where color consistency matters, define the target chromaticity and permitted tolerance, then retain instrument data with the approval. See the SDCM and bin-control guide.
Heat and mounting conditions
Operate the sample in the mounting condition that the product will see. A short strip lying on a metal bench does not represent a long strip enclosed in a shallow channel. Record the profile, diffuser, ambient condition, run length and operating time.
Do not convert one sample temperature into a universal life claim. The result is a comparison under stated conditions. Higher-power products may require a suitable aluminum profile or other thermal design; confirm that requirement for the exact model.
Mechanical handling
Check whether the strip fits the proposed channel and connector, bends within the permitted direction and radius, and can be cut and terminated without damaging pads or sealing. Test the planned installation process, not an improvised demonstration.
Adhesive performance depends on the substrate, cleaning, pressure, temperature, dwell time and environmental exposure. Approve the mounting system—tape, clips, profile or combination—rather than judging adhesive by peeling a fresh sample from one unknown surface.
Approve the complete system, not an isolated reel
Many field failures come from interfaces between components. Connect the proposed strip to the actual or approved equivalent:
- constant-voltage driver or high-voltage rectifier;
- dimmer and controller;
- amplifier, where used;
- wire size and representative cable length;
- connector and feed cable;
- aluminum profile and diffuser;
- end cap, sealant and cable entry for protected assemblies.
Run the modes the customer will use: full output, minimum approved dim level, fades, color changes and simultaneous channels. If the project uses long runs or multiple branches, build a representative mock-up or validate the design calculations before approval. The multiple-strip power-supply guide covers branch loading and feed layout.
For mains-voltage products, use qualified personnel and the product-specific accessories and instructions. A visually similar plug or connector is not evidence of electrical or sealing compatibility.
Use clear approval decisions
Finish with one of three decisions:
Approved
The sample and approval pack meet the stated requirements. Both parties sign or otherwise control the revision, and a retained reference is sealed and identified.
Conditionally approved
Only use this when the remaining changes are specific and measurable—for example, replace the temporary cable with the approved length, correct one artwork item, or supply a missing report before production. State who closes each point and whether another physical sample is required.
Rejected
List each failed requirement and the evidence. Avoid comments such as “quality not good.” Write the measured or observed difference, test condition and required correction. A revised sample must receive a new identifier so it cannot be confused with the rejected version.
Never sign an unlabeled reel. Months later, neither side will be able to prove which PCB, LED bin, coating, cable or artwork it represented.
Carry the approval into production and shipment
Attach the approved specification and sample ID to the purchase order. Add a change-control clause requiring written approval before substitutions to LEDs, PCB, resistors, adhesive, silicone, wire, connectors, control electronics or packaging that can affect fit, appearance, installation or performance.
Then turn the approval into measurable production and inspection controls:
- confirm incoming materials against the frozen bill of materials;
- identify production and color-bin batches;
- keep first-article or line-start approval records;
- define in-process electrical and appearance checks;
- use a documented pre-shipment inspection plan;
- compare shipment samples with the retained reference under the same conditions;
- record approved deviations before goods are released.
The retained sample is evidence, not the entire quality plan. It works best alongside tolerances, batch records, test reports and a sampling procedure.
When requesting samples, send the target application, destination market, model or required construction, expected order quantity, controller and driver details, profile drawing, packaging needs and approval checklist through the quotation form. That gives the supplier enough information to send a sample that can genuinely represent the intended bulk order.
Catalog & Sourcing Note
This article is prepared from our current product catalog and B2B specification workflow. Electrical, waterproofing and installation requirements vary by model and market, so confirm the final specification and approved sample before ordering.
Discuss Your Specification